
BUYER QUESTIONS
Hydraulic valve machining — where a manifold actually leaks
Most manifold and valve body problems are not the dimension you can see on a general drawing check. They come from three places:
- a cross-drilled channel that breaks into a seal face and leaves a thin wall
- a port that sits off-centre in its counterbore, so the O-ring never seats evenly
- swarf or a raised burr left at a channel intersection
All three survive visual inspection and surface treatment, and then show up as a leak at the pressure test — after plating, packing and shipping.
That is why port locations, counterbores, seal faces and threads are treated as critical features on hydraulic work here. They are held to ±0.005 mm, cut and gauged to NPT, BSP or metric class fit, and internal intersections are deburred and checked before the part comes off the machine. Every part is measured on the CMM and ships with the measured values in the box — with a free FAI on your first order.
QUOTING
What we need to quote a valve body or manifold
Send what you have. Drawings are reviewed within 48 hours, and the quotes that take longest are almost always missing the same six items:
- port sizes and thread standard (NPT / BSP / metric)
- working pressure
- seal type (O-ring groove, face seal, fitting)
- material and grade
- quantity
- required surface finish
If the design is not frozen yet, a STEP file plus the working pressure is enough to start — we will tell you which of the six is still open instead of quoting around it.
ORDER SIZE
One piece or a few hundred — there is no minimum order
A single replacement block and a 500-piece run go through the same setup and the same inspection. Quantity changes the unit price, not whether we take the job.
Prototypes ship 5–7 business days after drawing approval; production runs about 14 days, DDP door-to-door in the EU and the US, with export, freight, customs and last-mile delivery on one invoice.
MATERIALS & FINISH
Material and finish choices for hydraulic service
303/304/316L stainless where corrosion resistance decides, 1045/4140 carbon and alloy steel where strength and pressure rating do, aluminum 6061 for weight-sensitive housings, brass for low-pressure fittings.
On rods and cylinder surfaces, hard chrome is the usual wear layer; on aluminum housings, Alodine (chem film) keeps electrical conductivity for grounding and bonding. Stainless parts are passivated, wear surfaces get electroless nickel, and seal faces are machined to the Ra your application calls for — Ra 0.4 µm on the faces we hold.
Technical Specifications
Capabilities at a Glance
Every number below is what we hold on your parts — CMM-verified, with free FAI on your first order.
| Tolerance | ±0.005mm on critical dimensions |
|---|---|
| Materials | 303/304/316L stainless for corrosion resistance, 1045/4140 carbon or alloy steel for strength, brass and aluminum 6061 for weight-sensitive designs. |
| Process | 5-Axis CNC Milling |
| Surface Finish | Passivation · Electroless Nickel · Bead Blasting · Polishing (available on request) |
| Inspection | CMM report with measured values · free FAI |
| Lead Time | Prototypes 5–7 business days; production 14 days DDP door-to-door. |
Buyer checklist
What to check before you order Valves & Hydraulics
Most quote delays on Valves & Hydraulics come from drawings that leave the material condition, the critical tolerances or the inspection documents open. These six points are confirmed before a price is issued.
- Material grade and condition: 303/304/316L stainless for corrosion resistance, 1045/4140 carbon or alloy steel for strength, brass and aluminum 6061 for weight-sensitive designs.
- Critical dimensions and the tolerance tied to them: ±0.005 mm is what we hold where the drawing marks a feature critical.
- Surface roughness per functional face: Ra 1.6 µm is a typical as-machined value, and finer finishes are quoted on request.
- Surface treatment and masking: Passivation · Electroless Nickel · Bead Blasting · Polishing (available on request)
- Quantity and delivery: Prototypes 5–7 business days; production 14 days DDP door-to-door.
- Inspection documents: a CMM report with measured values, a free first-article report on new parts, and material certificates on request.
Process window by part type
| Feature | Typical tolerance | Surface roughness | How it is verified |
|---|---|---|---|
| Valve bodies | ±0.005 mm | Ra 1.6 µm | CMM report, measured values |
| Hydraulic flanges | ±0.005 mm | Ra 1.6 µm | Free FAI on new parts |
| Manifold blocks | ±0.005 mm | Ra 1.6 µm | In-process check at each operation |
| Mating faces and bores | ±0.005 mm | Ra 1.6 µm | CMM plus roughness check |
- Valve bodies for Valves & Hydraulics are machined from 303/304/316L stainless for corrosion resistance, 1045/4140 carbon or alloy steel for strength, brass and aluminum 6061 for weight-sensitive designs and held to ±0.005 mm on critical dimensions.
- Hydraulic flanges are checked in process at every operation and ship with a CMM report of measured values.
- First articles for Valves & Hydraulics come with a free inspection report, and material certificates are available on request.
- Orders for Valves & Hydraulics start at one piece, because quantity changes the unit price rather than the process.
- The Dongguan plant that machines Valves & Hydraulics holds ISO 9001:2015 certificate 93726Q00307R001.
- Prototypes of Valves & Hydraulics ship in 5–7 business days, and production runs are quoted DDP with one invoice.
FAQ
Frequently Asked Questions
Can you machine from customer-supplied castings or forgings?
Yes. Supplied castings and forgings are fixtured and machined, and the same part can be produced from solid bar or plate. For prototypes and small batches bar stock is usually faster and cheaper — castings pay off when the geometry would otherwise waste material.
Is there a minimum order quantity for valve bodies or manifolds?
No minimum. Single pieces, repair batches and production runs go through the same setup and the same CMM inspection; quantity only changes the unit price.
How is a manifold checked before it ships?
Port locations and counterbores are measured on the CMM, seal faces are checked for flatness and surface finish, and threads are verified with thread gauges. The measured values go into the report that ships with the parts — free FAI on your first order.
Can you machine multi-port hydraulic manifold blocks?
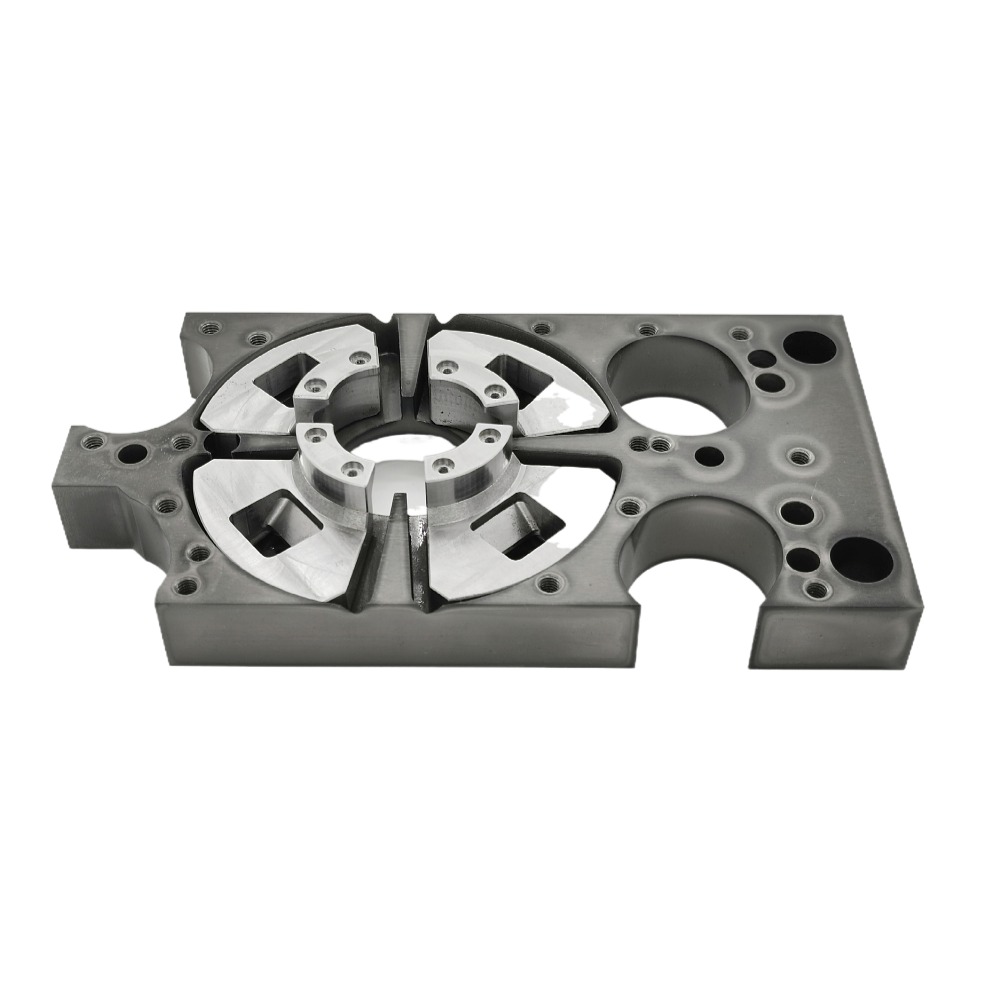
Yes. Multi-port manifold blocks with cross-drilled channels, plugged ports and custom porting are a core capability. We hold ±0.005mm on critical port locations and seal faces.
What thread standards can you produce?
NPT, BSP and metric threads in all common sizes, machined with thread form gauges. Threaded plugs and fittings are checked for class fit and leak-tight assembly.
How do you verify pressure-rated components?
Every part is CMM-inspected with report included; pressure test documentation is available on request. Seal faces are machined to the surface finish your application requires.
What materials do you recommend for hydraulic bodies?
303/304/316L stainless for corrosion resistance, 1045/4140 carbon or alloy steel for strength, brass and aluminum 6061 for weight-sensitive designs.
What surface finishes do you apply to valve components?
Ra 0.4μm on seal faces, passivation for stainless, electroless nickel for wear resistance. Blasting and polishing available per drawing.
How fast can you deliver valve prototypes?
Prototypes in 5–7 business days from drawing approval. Fast-track available on valve blocks and fittings when tooling is already proven.
Buyer Guide
Buyer's Guide
How to Get a Quote for Valve & Hydraulic Parts
Send the drawing with: port sizes and thread standards, working pressure, seal type, material, quantity, and required finish. Pressure requirements help us recommend the right grade and surface treatment.
Material Selection Guide
316L stainless for corrosion-resistant valve bodies, 4140 alloy steel for high-pressure manifolds, aluminum 6061 for weight-sensitive hydraulic components, brass for low-pressure fittings.
Machinability tips for Manifold Blocks
Keep port spacing generous for tool access, specify cross-hole plugging strategy early, and avoid sharp internal edges at channel intersections where stress concentrates.
Quality & Inspection
CMM inspection with full report on every order, measured values on critical dimensions, free FAI. Thread and seal-face dimensions are verified with dedicated gauges.
Lead Time & Shipping
Prototypes 5–7 business days, production 14 days DDP door-to-door. One invoice covers export, freight, customs and last-mile delivery to EU and US.
PRICING
What drives the price of Valves & Hydraulics
Valves & Hydraulics is quoted from the drawing, not from a catalogue: material block size, how many setups the geometry forces, the tolerance class and the batch size set the unit price. Machine-hour rates, material block prices and indicative bands at 1, 10 and 100 pieces are published in our CNC machining cost breakdown, so the number can be checked before a drawing is sent. A drawing review returns a quotation within 48 hours, with no minimum order quantity.
Get a Quote for Valves & Hydraulics
Send us your drawing — we review within 48h and return a quote with lead time.
Get a Quote →